- Industrial Heating Solutions
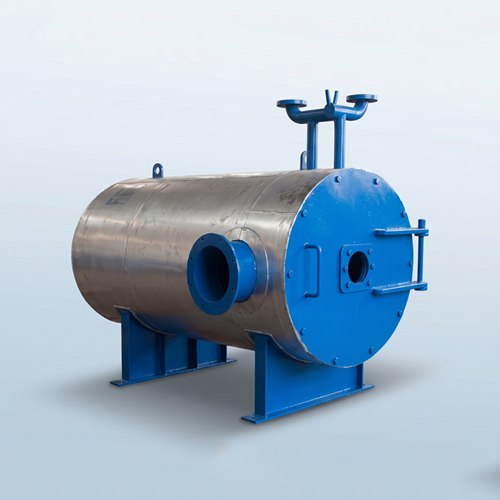
THERMIC FLUID HEATER
- The FBC Fired Thermic Fluid Heating System is designed for efficient and reliable heat transfer in industrial applications. The system comprises a radiative heat exchanger coil, convective heat exchanger coil, heat recovery unit (HRU), air pollution control equipment, controlled fans, and a dedicated thermic fluid pump.
- The thermic fluid is circulated by the pump through the convective and radiative heat exchanger coils to deliver heat to the final process.
- Flue gas flows from the furnace through the radiative and convective exchangers, then passes to the HRU and air pollution equipment before being drawn by the I.D. Fan to the chimney.
- The system ensures effective heat recovery, cleaner emissions, and long service life, making it a dependable choice for continuous industrial heating operations.
Capacity Range
1,00,000 Kcal/hr to 60,00,000 Kcal/hr
High-Capacity Performance
Suitable for a wide range of industrial heating applications.
Temperature Range
UP to 280°C
High-Temperature Performance
Designed to deliver hot air across a wide range of industrial heating requirements.
Ideal for various industries, including chemical, textile, pharmaceutical, food processing, oil and gas, and more.